Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier
Stop premature bearing failures in slurry-heavy mining operations with the right Bearing Seals for Wet Environments. Standard labyrinth seals fail under pressure, while Taconite designs use active grease purging to physically reject contaminants. Choose multi-layer barriers to eliminate unplanned downtime and reduce total lifecycle maintenance costs.
 Written by
author
- Published on
- 8 min read
- Updated

Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier
More labyrinth grooves do not equal better sealing in slurry.
In heavy wash plants and slurry-heavy mining operations, standard labyrinth seals fail because they lack active pressure. Taconite seals are mandatory for these environments due to their multi-layer physical barriers and active grease purging mechanism, which physically reject contaminants rather than merely resisting them.
I still remember the sweltering, mud-soaked atmosphere of a wash plant at a gold mine in Ghana. We had specified standard labyrinth seals for the vibrating screen bearings, operating under the assumption that the non-contact design would handle the constant slurry splash. It was a costly miscalculation. Within weeks, water and fine grit bypassed the labyrinth paths, contaminating the lubricant and seizing the bearings. The entire production line halted for a teardown that cost far more than the initial savings on seal components. That failure taught me that in wet environments, passive resistance is insufficient. You need active rejection. [NEED_CITE: common failure modes in mining vibrating screens per ISO 15243]
This experience drives how I approach specification today. When clients ask about sealing solutions for wet conditions, I do not just quote part numbers. I walk them through the physics of contamination ingress. Understanding why standard designs fail is the first step to selecting the right Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier partner who can provide genuine, traceable components for critical infrastructure.
What Defines a “Wet Environment” in Heavy Industry?
Water exposure is not binary; it is a spectrum of contamination severity.
In general manufacturing, a “wet environment” might mean occasional washdowns or high humidity. In heavy industry, particularly mining and aggregates, it means continuous immersion in abrasive slurry. This distinction is critical because the sealing requirements change drastically once particulate matter is suspended in the water.
Slurry acts as a grinding paste. When it enters a bearing housing, it does not just displace grease; it abrades the rolling elements and raceways. Standard IP ratings often fail to capture this dynamic because they test against clean water, not abrasive mixtures. [NEED_CITE: limitations of standard IP ratings in slurry applications]
Consider a dewatering pump in a quarry. It faces continuous water exposure and high-pressure spray. A standard seal might keep bulk water out initially, but the micro-ingress of silt leads to rapid lubricant degradation. In contrast, a conveyor tail pulley in an aggregate plant deals with fine grit that becomes airborne and settles into bearing housings. Here, the threat is not just moisture but dry abrasion that turns into slurry upon contact with any residual humidity.
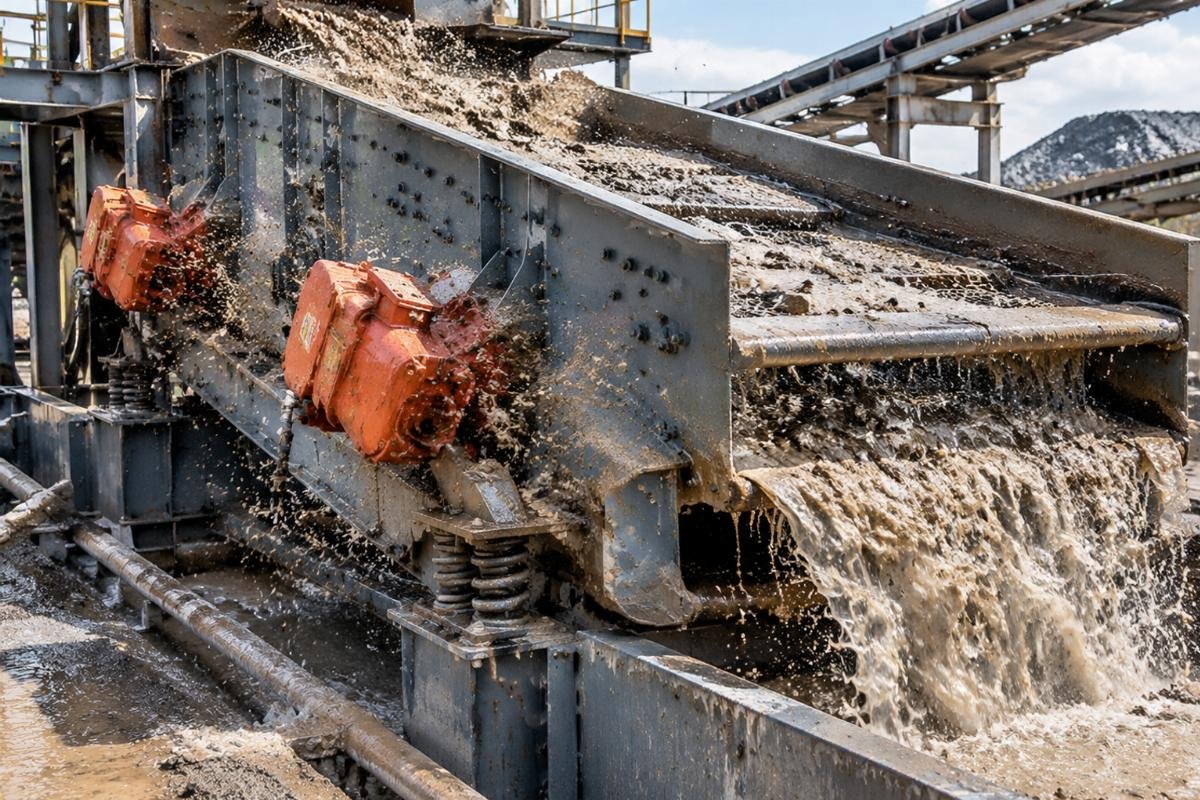
Defining the environment correctly dictates the seal choice. If you treat a slurry-heavy wash plant like a humid warehouse, you will face premature bearing failures. This is why sourcing from a knowledgeable Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier is essential. They must understand that “wet” in your context likely means “abrasive,” requiring a seal that can handle both fluid and solid contaminants simultaneously.
How Do Labyrinth Seals Actually Perform in Slurry?
Labyrinth seals rely on path length, but slurry bridges the gap.
The fundamental principle of a labyrinth seal is to create a long, tortuous path for contaminants to travel. By increasing the distance and adding turns, the seal aims to drop the pressure and trap particles before they reach the bearing. This works well for clean air or light dust. However, in wet environments, this passive design has a fatal flaw.
When slurry is present, the liquid carrier allows fine particles to flow through the labyrinth channels much faster than dry air would. Furthermore, if the pressure inside the housing drops due to cooling or operational cycles, the seal can actually suck contaminated fluid inward. [NEED_CITE: pressure differential effects on non-contact seals]
I have seen this repeatedly in aggregate conveyor applications. Operators install labyrinth seals expecting them to last for months. Instead, fine grit ingresses during every washdown cycle. The grit mixes with the grease, forming an abrasive compound that accelerates wear. The bearing does not fail immediately; it degrades quietly until seizure occurs, often taking down the entire conveyor system.

The misconception is that adding more grooves improves performance. In reality, without a positive pressure barrier, additional grooves just provide more surface area for slurry to adhere to. For mild moisture, labyrinth seals are cost-effective. But for any application involving direct slurry contact or high-pressure washdowns, they are vulnerable. This is where the limitations of a standard Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier inventory become apparent if they cannot offer upgraded alternatives.
Why Taconite Seals Dominate in Extreme Wet Conditions?
Taconite seals use active grease purging to create a positive pressure barrier.
The Taconite seal design was developed specifically to address the shortcomings of labyrinth seals in extreme environments. It combines a multi-layer labyrinth structure with lip seals and, most importantly, an active grease purging system. This system maintains a slight positive pressure inside the bearing housing, ensuring that any leak is outward, preventing contaminants from entering.
The multi-layer design includes primary and secondary barriers. The outer layer handles the bulk of the slurry, while the inner layers protect the bearing itself. The grease purging mechanism continuously flushes out any minor ingress, keeping the lubricant clean. [NEED_CITE: mechanics of positive pressure sealing in heavy-duty applications]
In a case involving a European wind farm operator facing salt spray and rain, switching to Taconite seals extended the service life of the main shaft bearings significantly. The active purging prevented salt crystallization inside the housing, which had been causing corrosion fatigue. The maintenance team reported that while grease consumption increased slightly, the reduction in unplanned downtime was substantial.

The key advantage is the active rejection of contaminants. Unlike labyrinth seals that hope contaminants get stuck in the grooves, Taconite seals actively push them away. This makes them the preferred choice for mining wash plants, dewatering pumps, and any machinery exposed to heavy slurry. When evaluating a Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier, look for those who can explain the grease purge volume calculations and multi-layer contact surface analysis, as these are critical for proper specification.
Labyrinth vs. Taconite: A Direct Specification Matrix
Choosing the right seal requires balancing initial cost against total lifecycle expense.
To make an informed decision, it is helpful to compare the two seal types across key performance indicators. The following matrix highlights the differences in protection level, maintenance requirements, and ideal applications. Note that the values are qualitative, reflecting typical industry observations rather than brand-specific proprietary data.
| Feature | Labyrinth Seal | Taconite Seal |
|---|---|---|
| Sealing Mechanism | Passive path resistance | Active grease purging + multi-layer barriers |
| Slurry Resistance | Vulnerable to bridging | Robust against abrasive ingress |
| Maintenance Frequency | High in wet environments | Noticeably reduced due to self-cleaning |
| Grease Consumption | Low | Moderate (due to purging) |
| Initial Cost | Lower | Higher |
| Ideal Application | Clean, dry, or mildly humid | Wash plants, slurry pumps, heavy mining |
| Failure Mode | Gradual contamination ingress | Rare, typically due to purge blockage |
[NEED_CITE: comparative maintenance costs in mining equipment per industry best practices]
The table shows that while Taconite seals have a higher initial cost and require more grease, they offer superior protection in harsh conditions. The “Vulnerable” rating for labyrinth seals in slurry reflects their tendency to allow particulate ingress when wet. Conversely, the “Robust” rating for Taconite seals acknowledges their ability to maintain integrity under continuous exposure.

For MRO managers, the decision often comes down to downtime costs. A seized bearing in a primary crusher can cost thousands in lost production. The extra grease cost for a Taconite seal is negligible compared to the expense of a teardown. This is why many OEMs are now specifying Taconite seals as standard for wet-end machinery. When sourcing from a Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier, ensure they can provide both types to match the specific severity of each application point in your facility.
How to Specify the Right Seal for Your Next Project?
Match the seal type to the specific contamination vector, not just the machine type.
Specifying the correct seal involves more than just knowing the bearing size. You must assess the nature of the contaminant and the operational dynamics. Start by identifying if the environment involves static moisture, dynamic splash, or submerged slurry. Each scenario demands a different level of protection.
- Assess Contaminant Type: Is it clean water, oily mist, or abrasive slurry? Abrasive slurries require Taconite seals. Clean water might be managed with enhanced labyrinth designs if pressure fluctuations are minimal.
- Evaluate Pressure Dynamics: Does the housing experience significant temperature changes? If so, breathing effects can suck in contaminants. Taconite seals with purge ports mitigate this risk. [NEED_CITE: thermal breathing effects in bearing housings]
- Calculate Grease Purge Volume: For Taconite seals, determine the required purge rate. Too little, and contaminants enter; too much, and you waste grease and create environmental issues.
- Verify Material Compatibility: Ensure the seal materials are compatible with the lubricant and the cleaning agents used in washdowns.
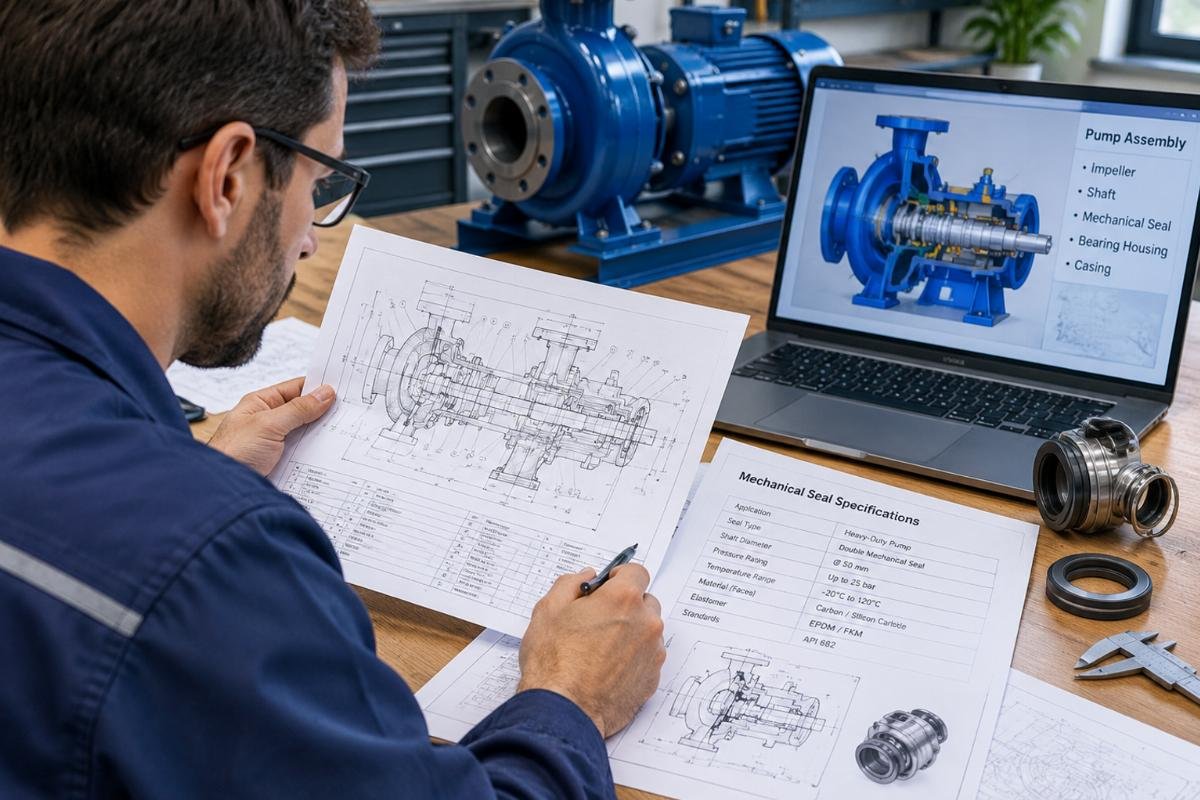
A Middle East steel mill once faced repeated failures in their water treatment plant pumps. They were using standard labyrinth seals. After switching to Taconite seals and optimizing the purge rate, the bearing life extended noticeably. The key was not just the seal type, but the correct specification of the purge system.
When working with a Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier, leverage their technical support. Ask for cross-brand equivalent model consultation and application guidance. A reputable supplier will not just sell you a part; they will help you analyze the failure mode and recommend the appropriate sealing solution. This collaborative approach ensures that you get the right component for the job, minimizing the risk of future downtime.
Conclusion
Passive sealing fails in active slurry environments.
Standard labyrinth seals are insufficient for heavy wash plants and slurry-heavy operations due to their inability to actively reject contaminants. Taconite seals, with their multi-layer barriers and grease purging systems, provide the necessary protection to prevent bearing failures and reduce unplanned downtime. Selecting the right seal requires a clear understanding of the contamination vector and operational dynamics. Partnering with a knowledgeable Labyrinth vs Taconite Bearing Seals for Wet Environments Wholesale Supplier ensures access to genuine, traceable components and the technical expertise needed for optimal specification.
Tags

About the author
author
Editor covering global sourcing, supplier verification, and industrial product knowledge. Content is compiled from manufacturer specifications, industry standards, and hands-on experience with international B2B buyers. Every article is fact-checked before publishing to help procurement professionals make informed decisions.
More articles by author